SLS, MJF and SLA each fit different production parts. Compare strength, finish, detail and size, and use five questions to pick the right process.
SLS, MJF and SLA each fit different production parts. Compare strength, finish, detail and size, and use five questions to pick the right process.
Tariffs, freight delays and minimum orders are pushing manufacturers to move low-volume parts closer to home. Here’s where US 3D printing fits and how to switch.
How SNL Creative uses AI agents to turn images into validated, print-ready full-color PolyJet jobs the same day, with automated geometry, validation, and J750 job setup.
Running the additive manufacturing lab at Faraday Future. Startup life to develop: fast iteration without losing traceability, machine commissioning built to certification standards, and a process that could keep up with an EV program changing week to week. That discipline now shapes how SNL Creative runs production 3D printing for automotive clients today.
Before SNL Creative, I built and ran the additive manufacturing lab at Faraday Future — commissioning machines and producing parts across the FF91, FF Zero 1, and LeSee programs. EV development moves faster and iterates harder than almost any other segment of automotive, and it forced a set of manufacturing disciplines that most 3D printing shops never have to learn. Here's what carried over into how we run production for automotive clients today.
Traditional automotive OEMs work on multi-year platform cycles with tooling budgets to match. EV programs — especially ones built from a clean-sheet platform like the FF91 — don't have that luxury. Battery packaging changes, thermal management requirements shift late, and interior architecture gets revised in response to weight and range targets almost until the day parts freeze. Injection tooling can't keep up with that pace. 3D printing can.
That environment teaches you things a slower program never will: how to hold dimensional consistency across dozens of design iterations, how to triage which parts genuinely need production-grade materials versus which are still validation prototypes, and how to keep a print floor running when the CAD underneath it is changing weekly.
Bringing EOS M400, M280, and Ampro systems online for Amaero's 10,000 sq ft LPBF facility — and doing it against AS9100 certification requirements from scratch — instills a specific kind of rigor: every machine parameter is documented, every material lot is traceable, and nothing goes into production until the process is proven, not just plausible. That same discipline is why SNL Creative operates as an ISO 9001:2015 certified shop today. It's not a box we checked for marketing; it's the standard we were trained to hold to at Faraday Future and Amaero before we ever printed a part for a client.
When a part is going into a vehicle that real engineers are betting a program on, you don't guess at material lot numbers after the fact. You track them from the start. That habit is baked into how we handle SLS powder management and every other material stream at SNL Creative — not because a client asked, but because we don't know how to run a floor any other way.
EV programs move fast, but "fast" at Faraday Future never meant skipping first-article inspection or ignoring a bad batch of powder. It meant building a process efficient enough that the rigor didn't cost you the schedule. That's the same balance we bring to automotive clients now: quick turnaround on functional prototypes and low-volume structural parts, without cutting the quality steps that make a part trustworthy.
For automotive and EV teams evaluating additive manufacturing, the highest-value applications tend to fall into a few consistent categories:
Engineering thermoplastics and industrial nylons (SLS, FDM, CFF) cover most of what shows up in automotive and EV development — from carbon-fiber-reinforced structural brackets to high-temperature under-hood housings. The right call depends on the load case, not just the geometry.
Running an AM lab inside a vehicle program teaches you the difference between a part that looks right and a part that's actually ready. That's the standard we hold every automotive project to at SNL Creative — whether it's a single validation prototype or a production run of structural components.
Upload your file for an instant quote, or reach out directly to talk through material selection, tolerances, and production volume.
A marketing calendar moves in days. Traditional manufacturing moves in months. That gap used to mean brands simply couldn't turn a viral concept, a limited-edition idea, or a piece of digital art into a physical product fast enough to matter. Additive manufacturing closes that gap — which is exactly why "drop" culture, pop-up activations, and virtual-to-physical collaborations have become one of the fastest-growing uses of 3D printing.
Injection tooling takes weeks to cut and thousands of dollars to commit to before you've made a single sellable unit. That math works for a product with a multi-year shelf life. It doesn't work for a limited-edition drop, a campaign tied to a single event, or a concept that needs to exist for exactly as long as the cultural moment does. Marketing teams increasingly need small batches, fast turnarounds, and the ability to change course after the first round of feedback — which is precisely the profile additive manufacturing is built for.
Limited-edition drops aren't a footwear-industry quirk anymore — they're a mainstream retail strategy. Luxury houses, sneaker brands, and consumer goods companies are all leaning into small-batch releases that create urgency, let a brand test an idea without overproducing, and give collectors something genuinely scarce. That model only works if production can match it: short runs, fast iteration, and finish quality high enough that "limited edition" doesn't look like a compromise.
It's not that brands suddenly want small batches — they always have. What's changed is that additive manufacturing now makes small-batch production genuinely cost-effective and fast enough to plan a real campaign around, instead of treating it as a novelty.
Some of the most interesting work happening right now starts as something that was never meant to be physical at all — a digital sculpt, an album's cover art, a piece of concept design built for a screen. Bringing that into the physical world used to mean handing it to a machinist who would "clean it up" for moldability, which almost always meant losing the thing that made it interesting in the first place.
Album artwork is designed for a cover, not a mold. Translating that visual concept into a physical object means preserving the exact intent of the digital design — proportions, texture, and detail that a traditional production process would flatten out. Additive manufacturing let the physical piece stay faithful to the original artwork rather than being redesigned around what a mold could produce.
This is the pattern behind virtual-to-physical work generally: a concept exists first as a render, a sculpt, or a piece of generative design, and the manufacturing process has to be flexible enough to catch up to the creative idea instead of forcing the idea to shrink down to what conventional tooling allows.
Working on campaign-driven or drop-based production has a different rhythm than a standard production order, and a partner who only knows how to run long, predictable batches will struggle with it:
| Standard Production | Drop / Marketing Production |
|---|---|
| Fixed, long-lead schedule | Compressed, often campaign-locked timeline |
| High volume, low per-unit cost focus | Low volume, high finish-quality focus |
| Design locked well before production | Design may still be evolving with creative or marketing input |
| Standard packaging | Often needs unboxing-grade presentation and finish |
| Public specs and sourcing | Frequently under NDA until launch day |
Marketing doesn't wait for tooling, and increasingly it doesn't have to. Whether it's a limited-edition collectible, a pop-up-exclusive object, or a digital concept that needs to exist in someone's hands for the first time, additive manufacturing is what lets the physical product move at the same speed as the idea behind it. SNL Creative brings the same in-house design, printing, and DyeMansion finishing capability to campaign and drop work that we bring to entertainment props and collectible design — under NDA when the project calls for it.
Tell us the launch date first — we'll tell you what's realistic and what it takes to get there.
SNL Creative’s technical paper on moving from prototype to high-volume 3D printed production. Covers batch consistency, repeatability tolerances by technology, material traceability, ISO 9001:2015 quality management, first-article inspection, and a checklist for qualifying a service bureau for production-grade additive manufacturing work.
The transition from additive manufacturing prototype to repeatable, high-volume production is one of the most under-documented challenges in modern product development. Engineers routinely achieve excellent prototype results — only to discover that the same file, printed at volume across multiple builds and machines, produces inconsistent parts.
This paper documents the systematic process controls, material qualification protocols, and quality management infrastructure that SNL Creative applies to every production engagement. Our ISO 9001:2015-certified quality management system (QMS) is the operational backbone of this process — not a marketing credential, but a living system of documented procedures, corrective actions, and continuous improvement cycles.
The core thesis of this paper: production-grade additive manufacturing is a managed process discipline, not a technology problem. The equipment is mature. The gap is almost always in process documentation, material traceability, and quality infrastructure.
This paper covers:
Most 3D printing service bureaus are optimized for prototyping. A single part, printed once, inspected visually, and shipped. This is not production. Production means the same part, printed to the same specification, across 50 or 5,000 units, delivered with traceability documentation that lets an engineer trace any non-conforming part back to its build, its material lot, its machine, and its operator.
ISO 9001:2015 is a process management standard, not a product standard. It does not specify tolerances or materials — it specifies that your organization must document its processes, establish measurable quality objectives, and demonstrate a systematic approach to identifying and correcting non-conformances. For additive manufacturing production, this maps directly to the failure modes above.
At SNL Creative, our QMS documentation covers machine calibration intervals, material receiving inspection, build parameter version control, first-article inspection protocols, and corrective action request (CAR) workflows. Every production job generates a job traveler that follows the part through every process step.
Production-grade additive manufacturing begins with qualified machines. A machine qualification protocol establishes the baseline capability of each system — its dimensional accuracy, surface finish repeatability, and mechanical property consistency — before any production work is assigned to it.
For multi-part builds, nesting strategy is a documented process step, not a technician judgment call. Our nesting guidelines specify minimum part-to-part clearance, prohibited zones near chamber walls, orientation rules for anisotropic materials, and maximum build density by material type.
| Parameter | SLS (EOS P396) | SLA (Neo 450) | FDM (Fortus 450mc) |
|---|---|---|---|
| Min. part-to-part clearance | 4 mm | 2 mm | 3 mm |
| Wall exclusion zone | 10 mm | 8 mm | 12 mm |
| Max. build density (vol.) | 35% | N/A (liquid) | N/A (FDM) |
| Preferred Z-orientation | Minimize Z-height | Feature-critical up | Minimize support |
| Thermal equilibration wait | 12–16 hr cooldown | Post-cure per spec | Chamber cool 30 min |
Material traceability is the documented chain of custody from raw material receipt to finished part. Without it, a batch failure cannot be root-caused, recalled, or prevented from recurring. Our ISO QMS requires that every production job references a specific material lot, and that all material lots are received, inspected, and logged before use.
| Material | Technology | Tensile Strength | Elongation | HDT | Key Application |
|---|---|---|---|---|---|
| PA2200 (Nylon 12) | SLS | 48 MPa | 18% | 163 °C | General production, snap fits |
| PA2241FR | SLS | 46 MPa | 14% | 163 °C | Flame retardant, EV / aerospace |
| TPU 1301 | SLS | 6.4 MPa | 340% | — | Flexible lattice, Digital Foam |
| ULTEM 9085 | FDM | 71 MPa | 5.8% | 153 °C | High-temp, aerospace-grade |
| ULTEM 1010 | FDM | 64 MPa | 3.3% | 216 °C | Highest temp FDM, autoclavable |
| Nylon 12CF | FDM | 115 MPa | 1.3% | 163 °C | Carbon-filled, structural |
| VeroUltra | PolyJet | 60–65 MPa | 25–35% | 49 °C | Color, fine detail, concept |
| Agilus30 | PolyJet | 1.4–3.1 MPa | 220–270% | — | Flexible, overmold simulation |
| Onyx (CFF) | CFF | 37 MPa | 1.7% | 145 °C | Base matrix for continuous fiber |
Lot numbers are recorded on the job traveler and retained for a minimum of 3 years under our ISO QMS document retention policy. In regulated-industry engagements (medical, aerospace), we can provide full material traceability documentation on request.
Dimensional repeatability is technology-specific and must be characterized for each machine-material combination. The tolerances below represent typical production capability at SNL Creative across qualified machines. They are not theoretical manufacturer specifications — they reflect actual measured performance on production builds.
| Technology | System | XY Accuracy | Z Accuracy | Min. Wall | Surface Finish (Ra) |
|---|---|---|---|---|---|
| SLS | EOS P396 | ±0.25 mm / ±0.1% | ±0.30 mm | 0.8 mm | 6–9 µm |
| SLA | Stratasys Neo 450 | ±0.10 mm / ±0.1% | ±0.10 mm | 0.5 mm | 1–3 µm |
| FDM | Fortus 450mc | ±0.20 mm / ±0.1% | ±0.20 mm | 1.0 mm | 10–16 µm |
| PolyJet | Stratasys J750 | ±0.10 mm / ±0.1% | ±0.10 mm | 0.6 mm | 1–2 µm |
| CFF | Markforged | ±0.20 mm / ±0.15% | ±0.20 mm | 1.2 mm | 8–12 µm |
ISO 9001:2015 certification means an accredited third-party auditor has verified that our quality management system meets the international standard for process control, continual improvement, and customer-focused quality management. For production clients, this means the following procedures are operational — not aspirational.
Every new production part receives a documented First-Article Inspection before full production release. The FAI package includes:
When a non-conforming part or batch is identified — whether in-process, at final inspection, or via customer return — our QMS triggers a formal non-conformance record. The workflow:
All production build files, machine parameter sets, and inspection records are version-controlled under our QMS document control procedure. A client can request the exact build parameters used for any job produced at SNL Creative within our retention period. This is critical for medical device and automotive applications where production records must be maintained for the life of the product.
Post-processing is not a cleanup step — it is a manufacturing process step that must be as controlled and documented as the print itself. Inconsistent post-processing is responsible for a significant share of production non-conformances in additive manufacturing.
| Process | System | Effect on Geometry | Effect on Surface | Tolerance Impact |
|---|---|---|---|---|
| Vapor smoothing | AMT PostPro3D | Minimal (<0.1 mm) | Ra: 9 µm → 0.4 µm | Specify pre-smooth dims |
| Dye finishing | DyeMansion DM60 | None | Color penetration ~0.1 mm | None dimensional |
| Bead blast | Manual | None | Matte, uniform | None dimensional |
| Powerfuse S (SLS) | DyeMansion | Minimal (<0.05 mm) | Glass-smooth surface | Account for material removal |
| Support removal (FDM) | Manual / bath | None | Witness marks possible | Post-removal inspection req. |
Critical-to-function surfaces that will receive post-processing must be identified in the design review. Nominal dimensions should be specified pre-post-process, with a documented expectation of the dimensional change introduced by each step.
Not all additive manufacturing service bureaus are equipped for production work. The following checklist represents the minimum qualification criteria that engineering and procurement teams should evaluate before committing a production program to an external 3D printing partner.
| Qualification Criterion | What to Ask | Red Flag |
|---|---|---|
| Quality certification | ISO 9001:2015 or AS9100 current? Third-party audited? | Self-declared quality, no external audit |
| Machine qualification records | Can you share dimensional accuracy data from your production machines? | No documented characterization data |
| Material traceability | How do you track material lots? What is your retention period? | No lot-level traceability |
| First-article inspection | Do you provide FAI packages? What is included? | Visual inspection only, no dimensional report |
| Non-conformance process | What happens when a batch fails inspection? | No formal process, handled case-by-case |
| Environmental controls | Is your facility temperature and humidity controlled? | No monitoring, no records |
| Production capacity | What is your machine uptime? What is your capacity utilization? | No data, or machines frequently unavailable |
| Post-processing traceability | Are post-process parameters documented per job? | Post-processing is informal or operator-driven |
High-volume 3D printed production is achievable — but only with the process infrastructure to support it. The technology is not the constraint. The constraint is documentation, traceability, qualification, and a quality management system that treats every build as a production event with a record, not a one-off service transaction.
SNL Creative has operated under ISO 9001:2015 since 2008 — not because our clients required it, but because we recognized early that the path to production-grade additive manufacturing ran through process discipline, not technology alone. Our equipment includes the EOS P396, Stratasys Neo 450, Stratasys Fortus 450mc, Stratasys J750, Markforged CFF systems, and Bambu Lab platforms, all operating under a unified QMS.
If you are evaluating SNL Creative for a production program, we welcome a process review call. We can walk through our QMS documentation, share qualification data for the technology relevant to your application, and provide sample FAI packages from comparable production jobs.
Product developers often face a critical choice: should they 3D‑print a component or invest in an injection mold? Each method has advantages and trade‑offs involving setup costs, per‑part pricing, lead time, design flexibility and scalability. This article compares the economics and timing of 3D printing versus injection molding, helping you decide which process suits your project.

Injection molding involves heating a thermoplastic or thermoset polymer and injecting it into a machined steel or aluminum mold cavity. Once cooled, the mold opens to release the finished part. This method is ideal for high‑volume production because the per‑part cost drops dramatically once the mold is built. However, creating the mold is expensive, requires skilled tool makers and can take several weeks. According to manufacturing experts, injection molds have a massive up‑front cost and long lead time—often tens of thousands of dollars and four to twelve weeks to machine a durable production mold. For prototyping, this investment rarely makes sense.
Additive manufacturing builds parts layer by layer directly from a digital model using FDM, SLA, SLS, MJF or metal powder bed processes. This eliminates the need for expensive molds, enabling rapid iteration and one‑off production. However, per‑part costs remain relatively high compared with high‑volume injection molding because each part requires machine time and material consumption.
Injection molding’s major cost driver is the mold itself. For a simple part, an aluminum prototype mold might cost $5 000–$20 000, while a high‑volume steel tool can cost $25 000–$100 000 or more. Conversely, 3D printing requires no specialized tooling; you pay only for material and machine time. This means you can start producing parts almost immediately. A study from Cad Crowd notes that injection molding becomes uneconomical for early prototypes due to high initial investment and long lead time. If you need just a handful of parts for testing, 3D printing is usually cheaper.
Once the mold is built, injection molding yields low per‑part costs—often pennies for small plastic components. 3D printing, however, has a relatively flat cost curve: the price per part remains roughly the same regardless of quantity. This is because additive processes do not leverage economies of scale; each part requires roughly the same amount of material and machine time. For example, producing 500 parts might cost $7 500 with 3D printing, while injection molding might cost $6 000 ($5 000 for the mold plus 500 × $2 per part). As volumes increase into the thousands, the savings from injection molding become even more pronounced.
Lead time is another critical factor. Injection molding projects typically require weeks to design, machine and test the mold. Any changes to part geometry necessitate reworking or completely remachining the tool, adding cost and time. 3D printing, on the other hand, can produce parts within hours or days. This agility allows for rapid prototyping, design iterations and short production runs. According to SNL Creative’s FAQ, standard prototypes can be turned around within 24–72 hours. If you need a small batch quickly or want to test multiple design iterations, additive manufacturing is unmatched.
3D printing excels at producing complex geometries, internal channels and lattice structures that would be impossible or prohibitively expensive to mold. With injection molding, parts must have draft angles and avoid undercuts to allow demolding. Incorporating complex features often requires slides, lifters or multiple part assemblies, increasing tool cost. 3D printing supports complex internal features and organic shapes without additional tooling. Therefore, for complex parts with low to medium volumes, additive manufacturing is often the better choice.

Determining the break‑even volume—the production quantity at which injection molding becomes cheaper than 3D printing—depends on material cost, part size and mold cost. A simplified approach is:
Break‑even quantity = (Mold cost) / (3D printing cost per part – injection molding cost per part)
For example, if the mold costs $10 000, and the 3D printing cost per part is $7 while the injection‑molded part cost is $2, the break‑even quantity is:
Break‑even quantity = 10 000 / (7 – 2) = 2 000 parts.
If your project requires fewer than 2 000 parts, 3D printing may be more cost‑effective. For larger volumes, injection molding’s lower per‑part cost will eventually offset the tooling expense.
Additive manufacturing can reduce material waste by building only the material needed for the part, whereas injection molding may waste excess material in sprues and runners. However, injection molding can use recyclable thermoplastics more easily than some 3D printing processes. The sustainability advantages of each method depend on the specific materials and production volumes.
Many companies use both techniques. They 3D‑print prototypes and low‑volume batches while refining the design; once demand justifies it, they invest in injection molds for high‑volume production. SNL Creative can support customers through this transition. Their design‑for‑manufacturing services help optimize parts for both processes, and their prototyping services offer quick turnaround times of 24–72 hours. When injection molding becomes viable, the company’s network of tooling partners can produce molds and continue production.
The choice between 3D printing and injection molding depends on quantity, budget, lead time and part complexity. Additive manufacturing eliminates tooling costs and shortens development cycles, making it ideal for prototypes and low‑volume production. Injection molding delivers low per‑part costs for high volumes but requires significant up‑front investment and longer lead times. By understanding the cost dynamics and design constraints of each process, you can choose the best manufacturing strategy for your product. SNL Creative’s expertise in both additive manufacturing and tooling support can help you navigate these decisions and scale your production efficiently.
Selecting the correct material is one of the most critical decisions in any additive manufacturing project. Whether you’re fabricating a one‑off prototype or ramping up to small‑batch production, your material choice affects mechanical properties, dimensional accuracy, surface finish, cost and overall part performance. In this guide we compare the most common materials—nylon 12, thermoplastic polyurethane (TPU), SLA resins, metal powders and carbon‑fiber‑filled composites—so you can make informed decisions for prototyping and production.
Additive manufacturing offers unmatched design freedom because it builds parts layer by layer. However, the base material still determines the strength, flexibility, thermal stability and biocompatibility of your final part. Getting the material wrong can lead to brittle prototypes, unexpected warping during printing or failure during use. Conversely, the right material can accelerate your project by eliminating costly rework and reducing time to market.
Selective Laser Sintering (SLS) and Multi Jet Fusion (MJF) often use Nylon 12. This thermoplastic is prized for its high strength‑to‑weight ratio and fatigue resistance—qualities essential for production components like housings, clips, brackets and machinery casings. In SNL Creative’s article on robotic grippers, the authors point out that SLS Nylon 12 offers excellent structural integrity and can withstand millions of gripping cycles. The ability to print support‑free internal channels also makes Nylon 12 ideal for complex geometries. Because SLS builds parts in a powder bed, there’s no need for support structures, which simplifies post‑processing.
For prototypes, Nylon 12 provides a good balance of rigidity and impact resistance. However, its relatively high cost compared with filaments like PLA or ABS means it’s best reserved for functional prototypes or production parts that require durability.
If flexibility or soft‑touch surfaces are required, thermoplastic polyurethane (TPU) is the go‑to material. In the same article about adaptive grippers, TPU is highlighted as providing elastic deformation that allows grippers to wrap around objects and absorb shocks. The material’s biocompatibility makes it suitable for medical devices and wearable products. TPU’s drawbacks include slower printing speeds and the need for careful parameter tuning to avoid stringing or poor layer adhesion. For prototypes, TPU allows realistic testing of flexible parts; in production, it is used for seals, gaskets and soft shells.
Stereolithography (SLA) and Digital Light Processing (DLP) use photopolymer resins cured by light. These technologies produce exceptionally smooth surfaces and high resolution, making them ideal for small parts, intricate details or models requiring tight tolerances. Common SLA resins include standard clear and opaque materials for display models, engineering resins for functional prototypes, high‑temperature resins for thermal resistance and biocompatible resins for medical devices.
However, SLA resins tend to be more brittle than thermoplastics, so they are usually reserved for prototypes, form‑fit testing or low‑stress applications. Post‑curing under UV light is mandatory to achieve full mechanical properties. If you need high gloss or clear finishes, SLA is unmatched, but for load‑bearing production parts, other materials may be better.
Metal 3D printing has become more accessible to small businesses thanks to bound‑metal deposition (BMD) and affordable powder bed systems. Industry forecasts note that desktop metal printers using BMD make structural metal printing possible for small engineering firms. Metals like 316L stainless steel, titanium alloys and tool steels enable production of high‑strength parts for aerospace, automotive and tooling applications. The materials are expensive and require post‑processing (debinding, sintering or hot isostatic pressing), but they can replace machined components where weight reduction or complex internal passages offer clear advantages.
Carbon‑fiber‑filled thermoplastics, such as PA12‑CF or composite nylon, combine nylon’s strength with the stiffness of continuous or chopped fibers. These materials are often used for jigs, fixtures and structural prototypes. They provide high stiffness, minimal creep and improved thermal stability but are abrasive to standard brass nozzles—special hardened nozzles are necessary.
| Material | Ideal applications | Notes |
|---|---|---|
| Nylon 12 (SLS/MJF) | Functional prototypes, housings, brackets, mechanical parts | High strength and fatigue resistance; support‑free printing; more expensive than standard filaments |
| TPU | Flexible seals, gaskets, medical devices, wearable products | Elastic deformation and shock absorption; slower printing; requires careful tuning |
| SLA resins | Models requiring smooth surfaces or high resolution, molds | Exceptional detail and surface finish; resins can be brittle; post‑curing required |
| Metal powders (BMD/PBF) | High‑strength end‑use parts, tooling inserts, heat‑resistant parts | Accessibility improving with desktop metal printers; high cost; requires sintering or hot isostatic pressing after printing |
| Carbon‑fiber composites | Jigs, fixtures, structural prototypes | Enhanced stiffness; requires hardened nozzles; may not be suitable for complex geometries if continuous fibers are used |
Material selection is the foundation of every successful 3D printing project. By understanding the unique properties of each material—strength, flexibility, resolution and cost—you can choose the right one for your prototype or production run. Industrial‑grade materials like Nylon 12 and composite nylons deliver the strength needed for load‑bearing applications, while TPU provides flexibility and shock absorption for soft touch parts. SLA resins offer unmatched detail for display models and intricate prototypes, and emerging metal printing technologies make steel and titanium parts accessible to small businesses. With careful material selection and SNL Creative’s design‑for‑manufacturing expertise, you can take your concept from idea to finished product with confidence.
The modern robotic gripper is no longer a rigid, one-size-fits-all tool. Consequently, the rise of additive manufacturing has completely reshaped how robots interact with complex objects. From delicate surgical robotics to high-speed factory automation, 3D printed solutions enable faster, cost-effective, and highly customizable designs.
Furthermore, whether you are developing a medical robotic gripper or optimizing an assembly line robotic gripper, 3D printing—specifically technologies like SLS (Selective Laser Sintering)—is unlocking new levels of flexibility.
A robotic gripper is an end-effector attached to a robot arm, designed to grasp and manipulate objects. In contrast to traditional rigid tooling, an adaptive gripper automatically adjusts its shape or force when interacting with objects. As a result, instead of complex programming for every unique item, these systems “adapt” in real-time through mechanical compliance.
This is especially important for adaptive grippers, which rely on flexibility and compliance to handle a wide variety of shapes.
An adaptive gripper is designed to adjust its shape or force automatically when interacting with objects. Instead of precise programming for every item, these grippers “adapt” in real time.
Beyond simple customization, additive manufacturing allows engineers to move past the limitations of CNC machining to create:
Compliant Mechanisms: Flexible joints that adjust to object geometry without extra motors.
Underactuation: Systems where fewer motors control multiple joints, reducing weight.
Rapid Prototyping: Iterating a custom design in days rather than weeks.
Complex Geometries: Integrating internal channels or lattice structures for light weighting and faster movement
This combination makes 3D printing the perfect match for adaptive technology.

In healthcare, precision is non-negotiable. Traditional metal grippers can damage delicate biological tissues, but 3D printed designs offer:
Examples of Use
3D printing enables rapid customization, which is crucial in medical environments where every patient is different.
Industrial manufacturing requires speed and durability. To address these needs, 3D printed grippers solve common bottlenecks by:
Reducing Tooling Costs: Eliminating expensive molds for custom parts.
Handling Irregular Components: Perfect for automotive or electronics assembly where parts vary in shape.
Faster Deployment: Swapping out end-effectors quickly to minimize line downtime.

The assembly line robotic gripper has evolved significantly with 3D printing, offering:
Benefits for Industry
This is especially valuable in industries like automotive, electronics, and consumer goods.
Similarly, adaptive grippers are the backbone of bin picking systems and warehouse automation. They allow a single robot to handle a high diversity of SKUs (Stock Keeping Units), ranging from heavy boxes to fragile, irregular packages.
Adaptive grippers are widely used in:
3D printed designs help handle:
While design is critical, performance failures often stem from poor material selection. To ensure production-ready results, the industry standard focuses on specific materials:
For the frame and load-bearing components of an assembly line robotic gripper, SLS Nylon 12 is the gold standard.
High Strength-to-Weight Ratio: Ideal for fast-moving robotic arms.
Fatigue Resistance: Withstands millions of gripping cycles.
Support-Free Printing: Enables complex internal geometries that are impossible to machine.
The “adaptive” nature of these grippers comes from flexible materials like TPU (Thermoplastic Polyurethane).
Elastic Deformation: Allows the gripper to “wrap” around objects.
Shock Absorption: Protects both the robotic system and the object being handled.
Biocompatibility: Specialized resins are available for medical robotic gripper applications requiring sterilization.
3D printing is often seen as a prototyping tool—but with the right materials, it becomes a production solution.
To maximize results:
Ultimately, a 3D printed gripper is only as reliable as the process used to create it. Therefore, success depends on a contract manufacturing partner who understands:
Tight Tolerances: Ensuring parts fit perfectly onto robotic arms.
Repeatability: Delivering the same quality across hundreds of batches.
Post-Processing: Achieving the surface finish required for industrial or medical environments.
The success of a production-ready robotic gripper ultimately depends on who makes it. A reliable contract manufacturing partner ensures consistent print quality, tight tolerances, and repeatability across batches, which is critical for both assembly line robotic gripper deployments and medical robotic gripper applications. They also bring expertise in material validation, post-processing, and quality control—areas where small inconsistencies can lead to performance failures. The right manufacturing partner doesn’t just produce parts—they safeguard the reliability, scalability, and real-world success of your adaptive gripper system. Anything less, and you’re leaving performance—and reliability—on the table.
In the competitive landscape of Unmanned Aerial Vehicles (UAVs), traditional manufacturing often hits a ceiling. When mission success depends on maximizing flight time and payload capacity, the “off-the-shelf” or CNC-machined approach is no longer enough. At SNL Creative, we function as your dedicated manufacturing partner, bridging the gap between advanced digital design and high-volume, flight-ready production.
By specializing in industrial additive manufacturing, we produce drone airframes and components that are lighter, stronger, and more complex than anything achievable through traditional tooling.
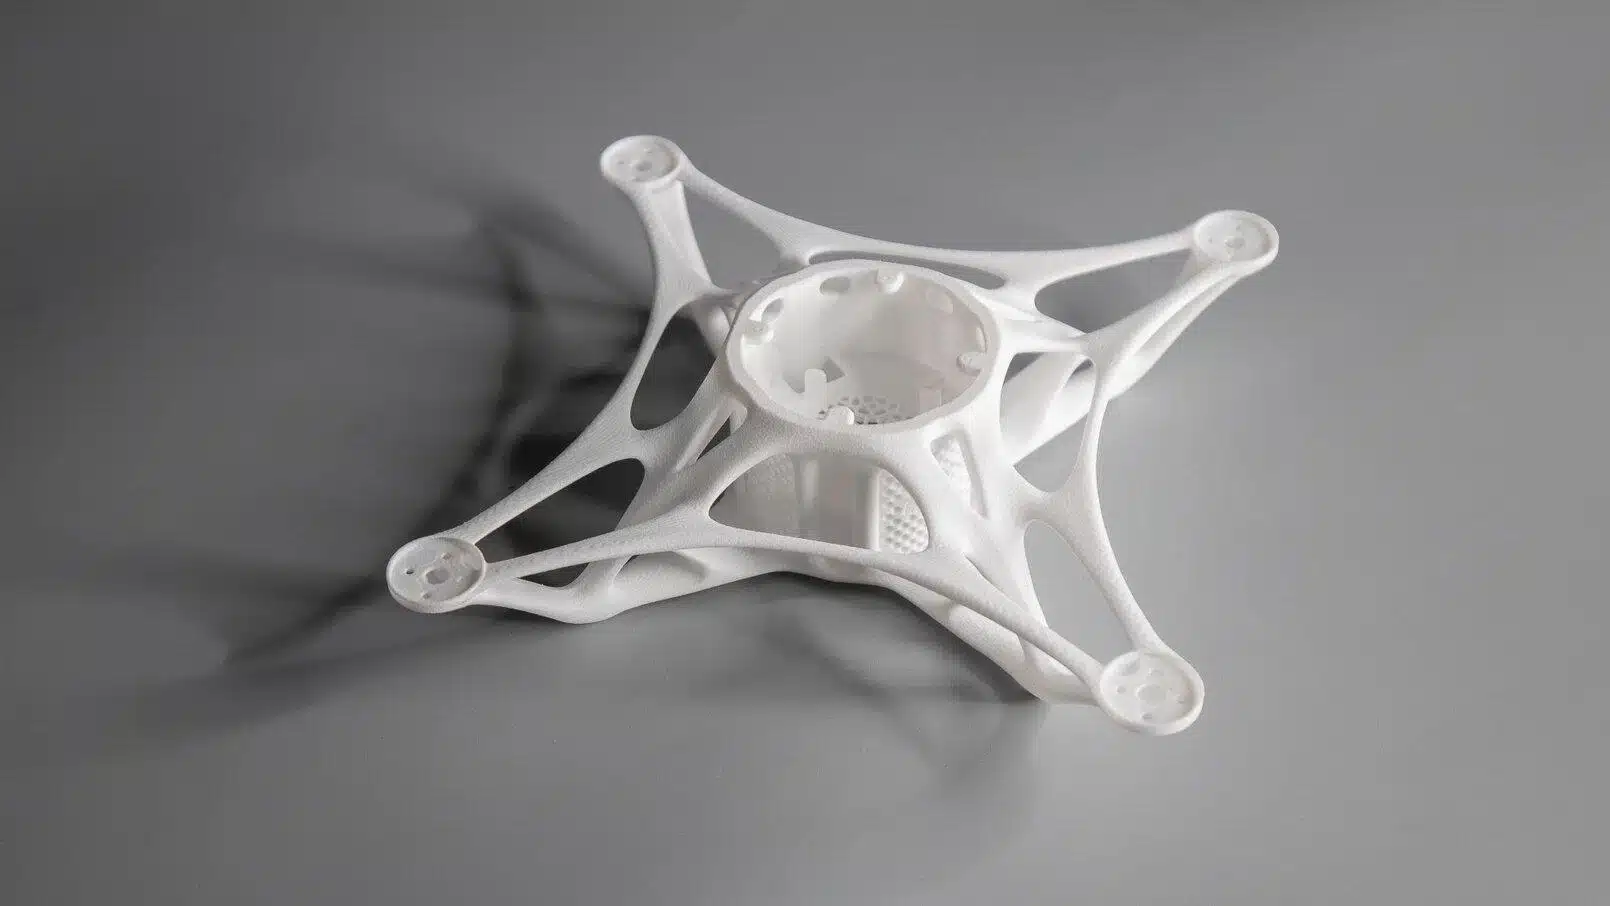
Weight is the ultimate enemy of flight. Selective Laser Sintering (SLS) has emerged as the definitive production method for aerospace partners looking to optimize structural geometry. As a manufacturing partner, SNL Creative utilizes SLS to move beyond the restrictive constraints of traditional molds.
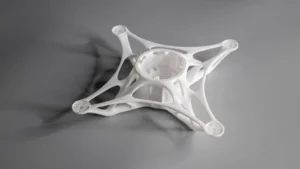
Part Consolidation: Unlike traditional manufacturing that requires multiple parts and heavy fasteners, we can print entire drone arms or chassis sections as a single, unified piece. This reduces potential points of failure and significantly lowers the overall weight of the assembly.
Hollow Structural Sections: We produce hollow components that maintain high torsional rigidity while minimizing mass. This allows for integrated internal airflow channels, which improve aerodynamics and provide dedicated cooling paths for internal electronics.
Integrated Lattice Ribbing: Our systems can produce internal lattice structures that act as the “bones” of the drone, providing extreme rigidity only where the flight loads demand it.
The durability of a UAV is only as good as the material it’s built from. We offer a specialized suite of high-performance materials designed to withstand the rigors of field operations, from desert heat to high-altitude cold.
Nylon 11 & 12 (SLS): These materials provide the impact resistance and UV stability required for end-use airframes. We also offer variants reinforced with Glass Beads or Carbon Fiber for projects requiring maximum stiffness and thermal resilience.
TPU 1301 (Digital Foam): A game-changer for drone components. We utilize TPU 1301 to create “Digital Foam” landing gear and internal housings. By varying the lattice density, we can program specific levels of energy absorption and vibration dampening to protect sensitive gimbal and camera equipment.
Multi Jet Fusion (MJF) Plastics: For robust housings and waterproof enclosures, our MJF production ensures exceptionally dense parts with isotropic strength—perfect for the “skin” of the drone and internal electronic bays.
Engineering-Grade FDM Filaments: Through systems like the Bambu Lab X1E, we run specialized filaments for components requiring high-temperature resistance or specific chemical properties.
SNL Creative is built to scale. We have transitioned 3D printing from a prototyping tool into a robust, mid-to-high volume production solution.
ISO 9001:2015 Certified Quality: Our Cypress, CA facility operates under a strict Quality Management System. This ensures that the 1,000th drone component we ship is as precise and reliable as the first.
Domestic Supply Chain Security: By partnering with a domestic manufacturer, you eliminate the logistical risks, long lead times, and intellectual property concerns associated with overseas production. We provide a localized, secure supply chain for defense and high-tech commercial applications.
Rapid Batch Iteration: One of the greatest advantages of our production model is agility. If field testing necessitates a design tweak—such as a new sensor mount or cable routing—we can implement that change in the next production batch without the sunk cost of expensive steel tooling.
A component isn’t flight-ready just because the print is finished. SNL Creative provides a comprehensive suite of finishing services to ensure your airframes meet professional standards:
Chemical Vapor Smoothing: Essential for aerodynamics, this process seals the part’s surface and reduces drag.
Tactical Coatings: We offer specialized dyeing and UV-protective coatings for environmental resilience.
Hardware Integration: Our production line includes installing threaded inserts and fasteners, delivering components ready for immediate assembly.
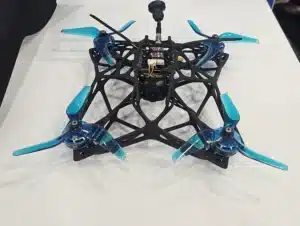
The transition from a conceptual design to a flight-ready fleet should be seamless. At SNL Creative, we combine the speed of additive manufacturing with the discipline of industrial production.
Whether you are developing a new delivery platform or a specialized reconnaissance UAV, we have the materials and the certifications to bring your production to life.
[Get an Instant Quote] today to see how our costing API can streamline your workflow, or contact Shawn and the production team to discuss your specific material requirements and volume needs. Let’s build the future of flight together.
Locations we Serve;